
Ceramic Fiber
Ceramic Fiber Plus Blanket
Blanket with lower shot content and higher tensile strength for demanding linings and modules.
Rotary kiln backing, preheater cyclones, clinker coolers and ducts. Calcium silicate and rock wool for alkaline, dust-laden service.
Overview
Cement manufacturing is a continuous, energy-intensive process where maintaining thermal efficiency directly impacts production costs. From the preheater tower and rotary kiln to the clinker cooler and ductwork, every component requires reliable insulation engineered for high-temperature alkaline environments with abrasive particulate-laden gas streams.
Rosetexwool supplies advanced insulation systems for cement plants worldwide. Our microporous nano boards provide ultra-thin hot-face insulation for kiln shells, while calcium silicate boards and rock wool blankets cover preheaters, coolers, and extensive ducting networks.
Three conditions decide whether an insulation system survives a cement line, and none of them appears on a product data sheet. Alkali vapour from the raw meal attacks binder and shot at sustained temperature; dust-laden gas abrades anything exposed on preheater risers and tertiary air ducts; and the steel shell has to stay cool enough that it does not creep or ovalise under its own load. A material can pass its temperature rating and still fail on all three.
We therefore match grade to zone rather than to a single maximum figure: high-purity ceramic fiber in the burning zone, calcium silicate where the shell needs rigidity and dimensional stability against vibration, and hydrophobic rock wool on cooler casings, duct runs and plant buildings, where dewpoint and condensation, not peak temperature, drive the failure.
Material Options
Cement plants run some of the hottest, most abrasive process equipment in industry. Choosing insulation means balancing kiln-zone temperature, alkali attack and cost. How rock wool compares with the materials specified across cement production lines:
| Material | Service temperature | Fire rating | Thermal conductivity | Relative cost | Key use in cement plants |
|---|---|---|---|---|---|
| Rock wool | -200 to 650°C | A1 non-combustible | 0.032-0.040 W/(m·K) | Low | Equipment foundations, duct wraps, fire barriers |
| Ceramic fiber | up to 1260°C | A1 | ~0.03 | Higher | Kiln & preheater linings, hot-air ducts |
| Calcium silicate | up to 1100°C | A1 | ~0.05-0.07 | Medium | Rigid kiln-shell backing, duct & vessel insulation |
| Glass wool | up to 400°C | A1 | ~0.04-0.05 | Low | Low-temp pipe & building insulation |
| PU / PIR foam | -50 to 150°C | B1/B2 | 0.022-0.027 | Medium | Thermal-only; needs fire barriers |
For most cement-plant insulation rock wool delivers the best balance of cost and A1 fire safety at up to 650°C; ceramic fiber lines the hottest kiln and preheater zones above 800°C, while calcium silicate adds rigid, alkali-resistant backing on kiln shells and large ducts.
Kiln
The rotary kiln is the one unit where refractory and insulation are the same decision. The shell is a steel cylinder turning at 3 to 5 rpm; inside it the burning zone runs at 1,400 to 1,500 °C on the material side. What protects the shell is not the brick alone but the clinker coating that freezes onto the brick face, and that coating only stays put while the shell temperature underneath is stable.
This is why shell temperature is the number operators actually watch. A hot spot above roughly 400 °C means the coating has dropped off, the brick is wearing fast and the shell is starting to ovalise. A backing layer behind the brick lowers shell temperature, which widens the window in which a coating can form and survive — that is the whole value of insulation on a kiln.
Preheater
A five-stage preheater is a vertical sequence of cyclones in which raw meal meets hot gas: gas enters the bottom stage around 800 to 900 °C and leaves the top stage near 350 °C. The gas path is abrasive, and the material path is worse — risers and dip tubes are eroded from the inside by dust moving at 20 m/s and more.
Insulation here does two jobs: hold the gas temperature so the calciner still gets the heat it was designed around, and keep the steel casing below the temperature at which it starts to creep. Modules on the riser and calciner vessel, with ceramic fiber or calcium silicate on the tertiary air duct, cover both.
Clinker Cooling
The grate cooler takes clinker at 1,300 to 1,400 °C down to roughly 100 °C above ambient, and the air it uses becomes secondary and tertiary combustion air. Its casing is one of the few surfaces in a cement plant where insulation pays back through combustion efficiency rather than through shell protection.
The constraint is abrasion on the outside and vibration on the inside. A board that stays in contact under both is worth more than one with a better conductivity, which is why rigid calcium silicate and dense rock wool board are the usual answer here rather than blanket.
Waste Heat Recovery
A suspension preheater boiler takes gas at 300 to 400 °C from the preheater outlet, and an AQC boiler takes hot air from the cooler. Together they can carry a quarter to a third of the plant's electrical demand without burning any additional fuel.
The insulation duty is unglamorous and decisive. Economiser and boiler walls are lined with ceramic fiber, lower-temperature headers and steam piping are wrapped in rock wool, and every duct on the way to the boiler is sealed so the gas still arrives at design temperature. A 20 °C drop along that path is generation the plant paid for and never received.
Ducts & Stacks
Kiln exhaust and dedusting ducts are long, large-diameter and mostly outdoors, which makes them the largest insulated surface area in the plant. The failure mode is rarely heat loss — it is condensation. Flue gas carrying SO₃ has an acid dewpoint around 120 to 150 °C, and any section that drops below it corrodes from the inside of the shell outwards.
Size the insulation to hold the steel above the dewpoint at the lowest expected load, not at full firing. On tail-end ducts and stacks that usually means more thickness than the heat-loss calculation alone would call for.
Energy Case
Specific heat consumption on a modern dry-process line sits around 2,900 to 3,300 kJ/kg of clinker. Insulation cannot change the chemistry, but it does change how much of that heat leaves through a steel surface before it ever reaches the material.
Two numbers frame the calculation. Shell temperature: 250 to 300 °C on the kiln shell is normal, and anything sustained above 350 °C is a maintenance signal rather than an insulation problem. Surface loss: every square metre of bare 300 °C shell is a permanent fuel cost, and the economic thickness follows from fuel price and operating hours, not from a catalogue.
EN ISO 12241 covers the steady-state case. On the kiln itself the calculation is secondary: the lining is designed for campaign life, and the insulation exists to keep the shell cool enough that the campaign is achievable.
Installation
A cement plant is a vibration and abrasion environment, and most lining failures start at a fixing rather than at the hot face.
Standards
Cement plants mix refractory specification on the hot side with ordinary industrial insulation everywhere else:
Selection Guide
Material choice follows zone temperature: above 800°C ceramic fiber is specified for the kiln and preheater; for 300–800 °C rock wool offers the best cost-performance with integrated fire safety; in alkali- or moisture-exposed areas calcium silicate delivers chemical stability. Rosetexwool supplies cut-to-size blankets, boards and modules with jacketing suited to the dusty, high-temperature cement environment.
Related Applications
Cement and lime kilns run at sustained high temperatures. Related high-temperature process applications:
Recommended Products
Matched to this application's temperature range and service conditions.
Blanket with lower shot content and higher tensile strength for demanding linings and modules.
Rigid calsil board to 1100 °C for furnace and kiln linings. High compressive strength.
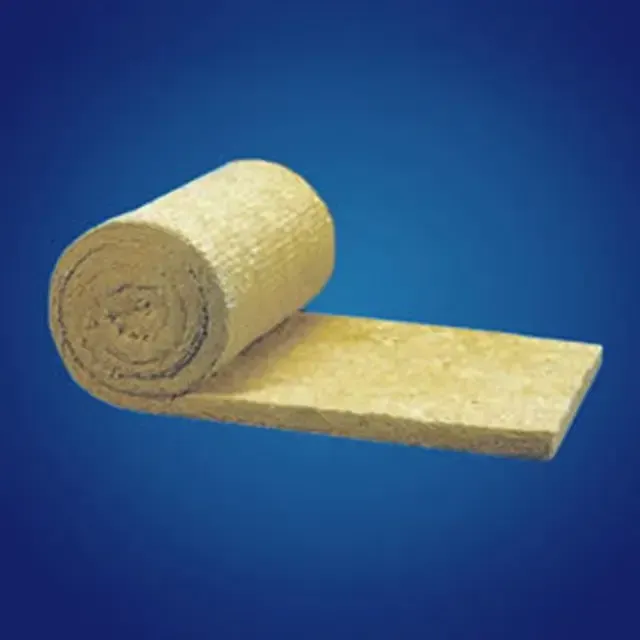
Flexible rock wool blanket to 650 °C for tanks, large ducts and equipment. A1 non-combustible.
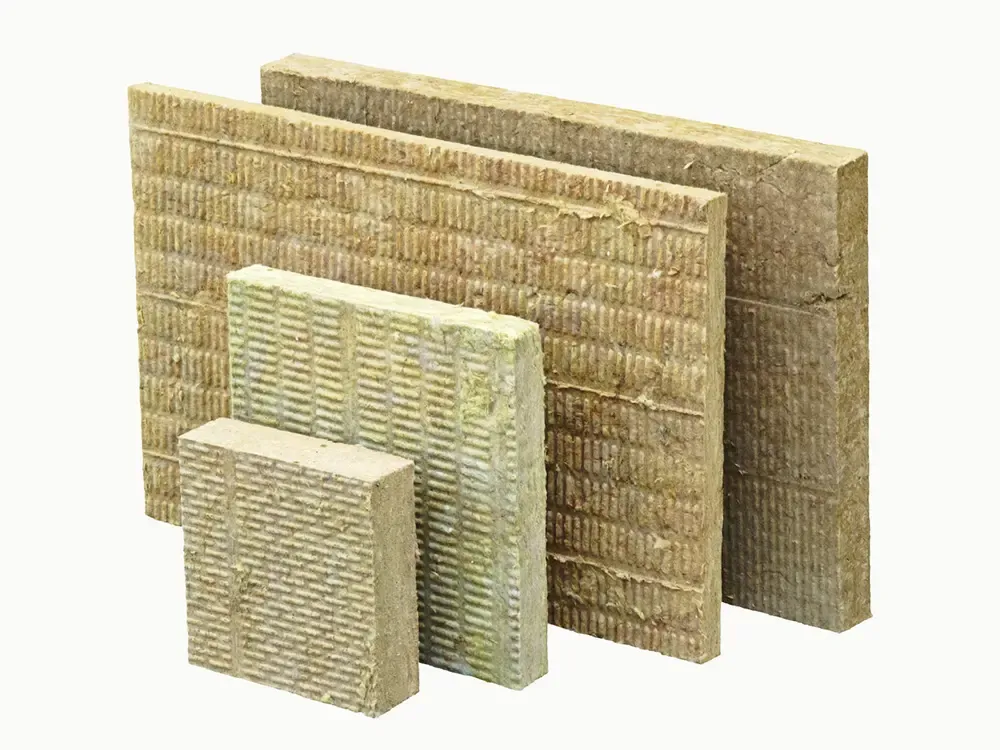
Basalt board to 650 °C. Fire-safe, water-repellent, for walls, roofs and oven casings.
Why Rosetexwool
Why Cement operations choose Rosetexwool insulation solutions.
Nano insulation on kiln shells lowers shell heat loss, directly reducing coal or gas consumption per ton of clinker.
Lower shell temperatures protect kiln tires and support rollers from overheating and premature wear.
Reduced surface temperatures in preheater towers and cooler buildings improve working conditions.
Durable, properly specified insulation extends equipment life and reduces unplanned maintenance.
Support
We recommend microporous nano insulation boards for the burning zone, which can reduce shell temperatures by 50–80 °C in just 5-10mm thickness. For the transition and safety zones, ceramic fiber blanket with stainless steel cladding is a proven solution. Both options minimize added weight on the kiln shell.
Yes. Our calcium silicate boards are inherently resistant to mildly alkaline environments. For preheater cyclones and ducting exposed to heavy dust-laden gas, we recommend hydrophobic rock wool with full metal cladding to prevent dust ingress into the insulation layer.
Yes. Our kiln shell insulation systems use mechanical fastening with stainless steel banding and welded studs to withstand continuous rotation and vibration. We provide complete installation guidance including stud pattern recommendations for your kiln diameter and RPM.
Last updated: November 6, 2026
Ready to start? Tell us your specs — we'll quote within 24 hours.
Get pricing
Tell us about your cement project requirements — our team responds within one business day.
Free sample + 24-hour engineering quote
Spec-match guarantee